Halal Cattle Slaughter Line | 20-500 heads/day
Halal Cattle Slaughter Line Designed Around Certification Review
Zhengye designs halal cattle slaughter lines for abattoirs that must satisfy religious, veterinary and hygiene audits at the same time. We engineer the restraint, killing, bleeding, dressing and separation systems as one coordinated line, then provide the drawings and documentation your certification body needs to review.
The equipment does not certify a plant by itself. Final halal approval remains with the recognized authority in your country. Our role is to make the physical line, process flow and project documents consistent with the requirements those authorities inspect.
What Changes in a Halal Cattle Line
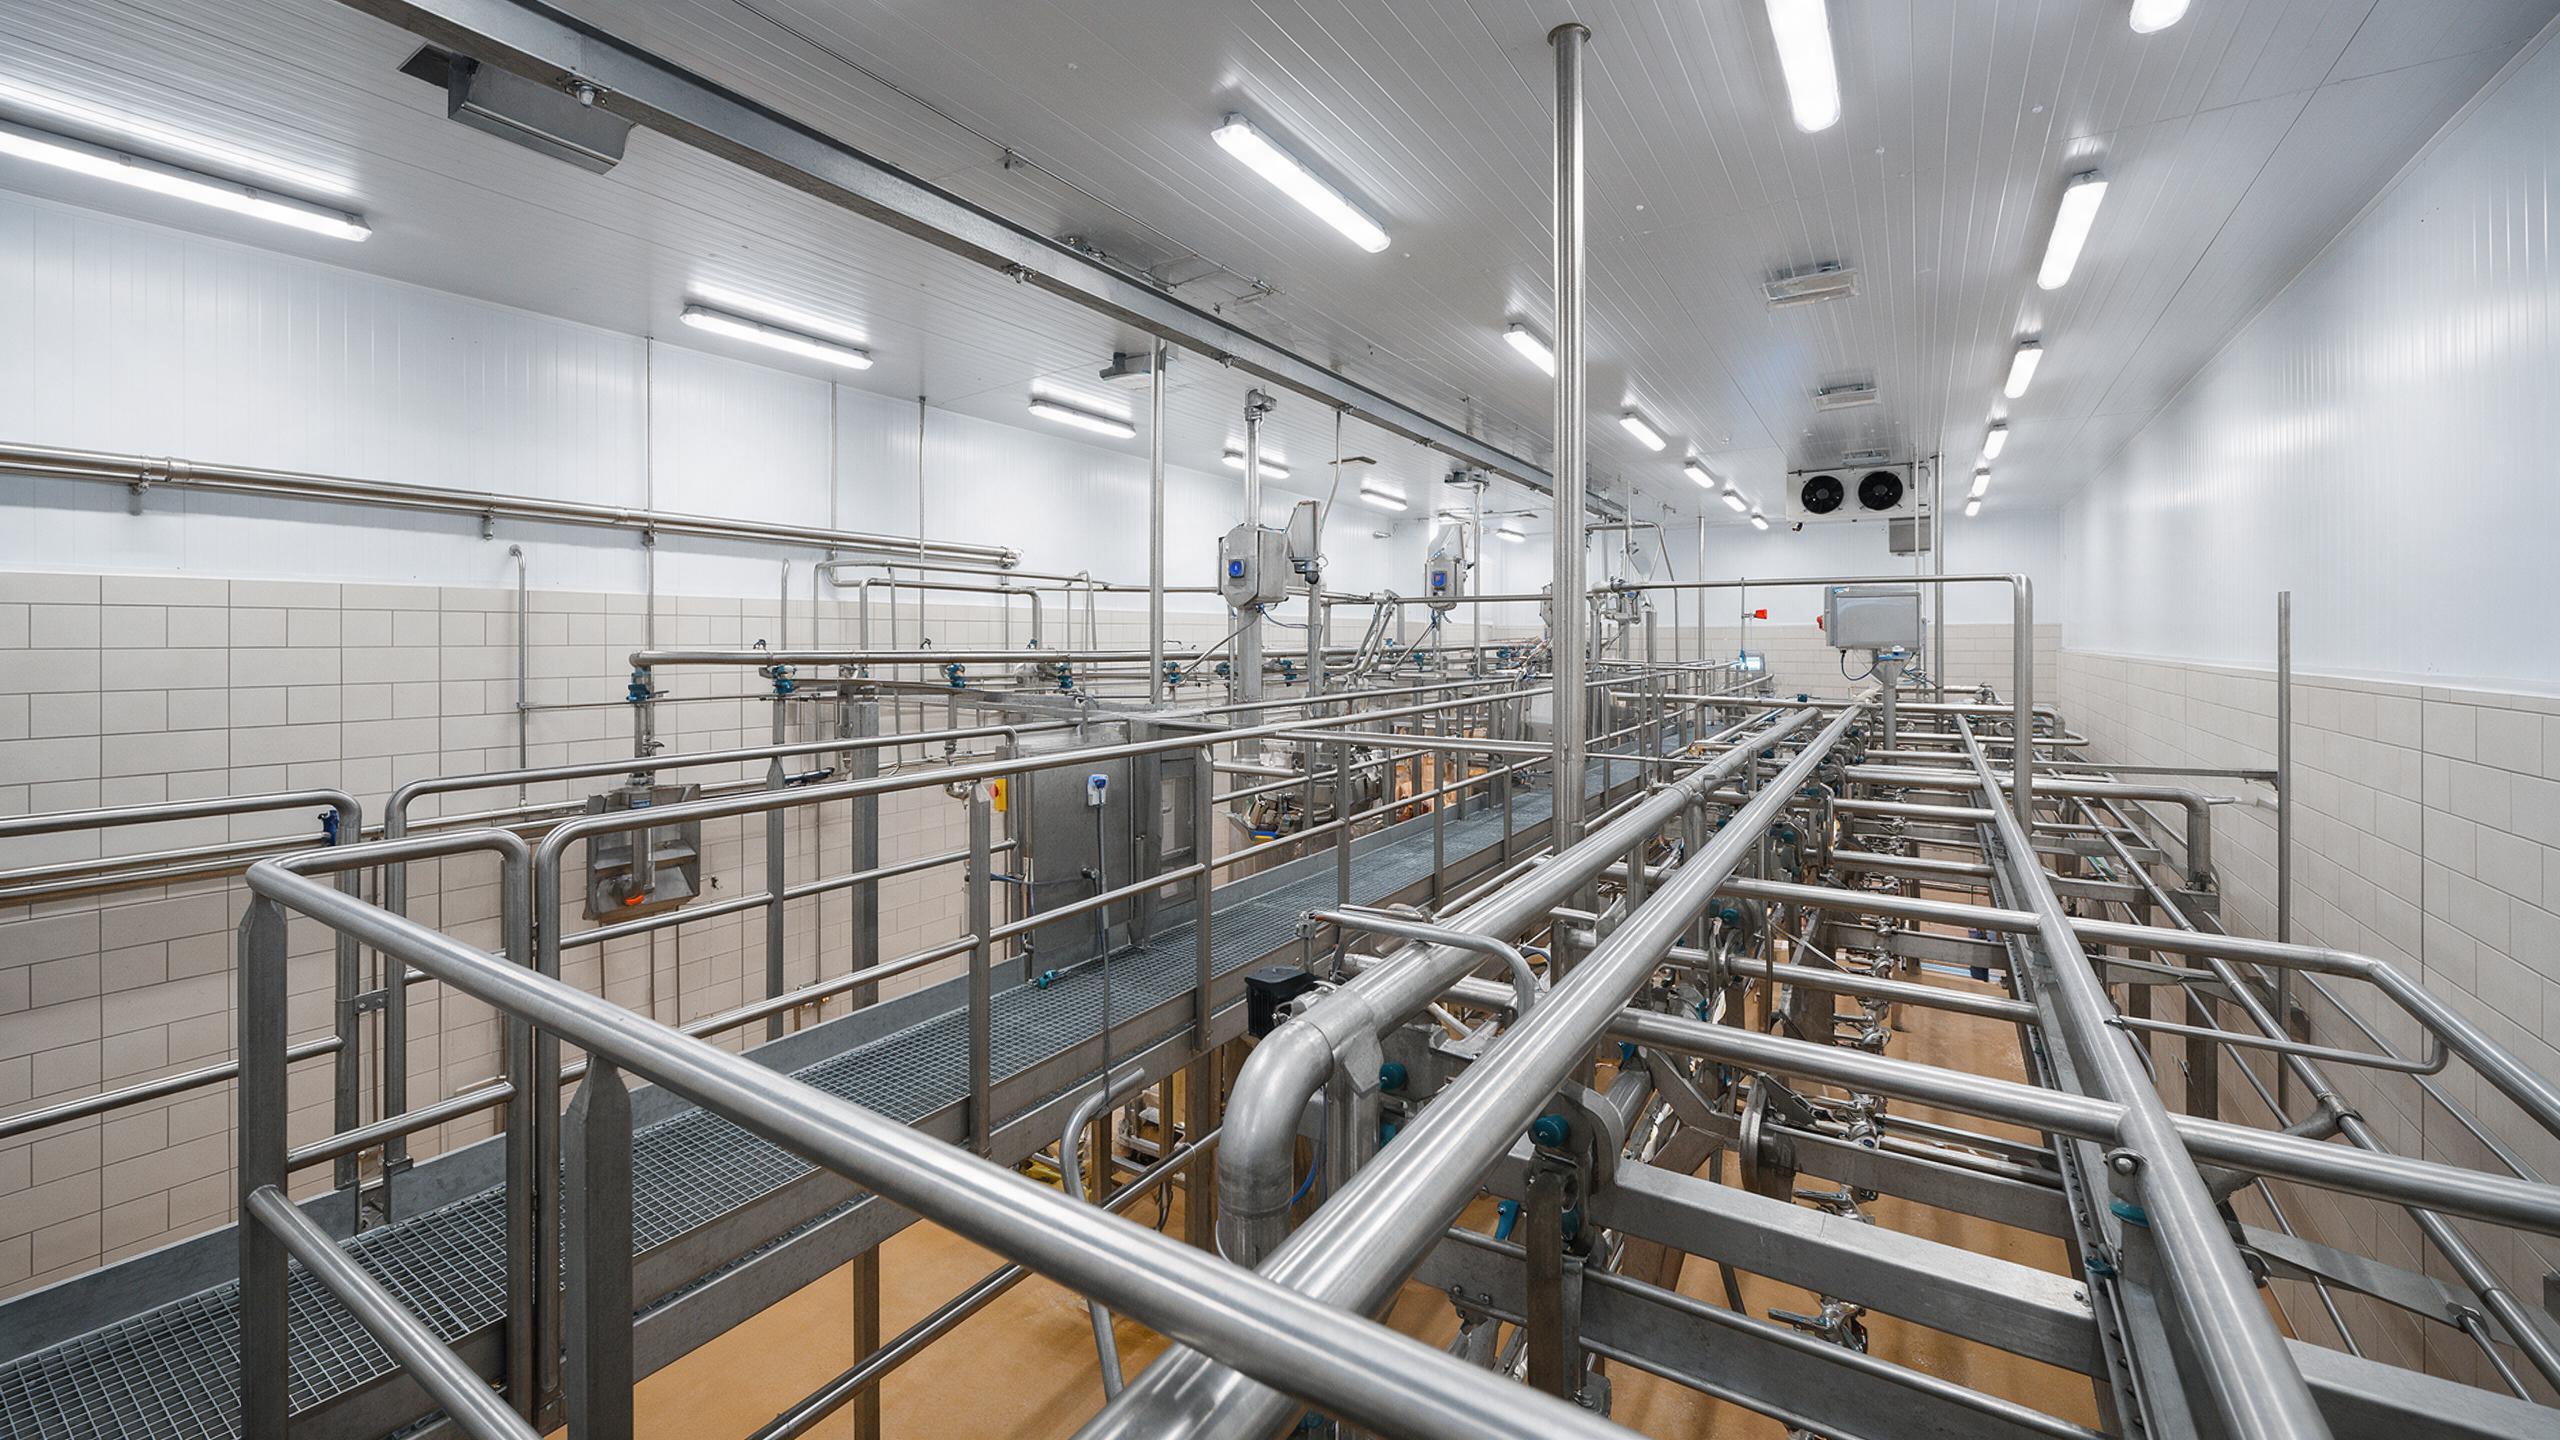
A halal cattle line shares most stations with a conventional line, but the front end and the segregation strategy are not interchangeable. The animal must be presented and restrained so the slaughterman can make the required cut without obstruction. The bleeding rail must provide enough time and uninterrupted travel for complete exsanguination before dressing begins. The layout must prevent cross-contact between approved and non-approved material, and the documentation must allow an auditor to trace equipment, cleaning and process control.
Front-End Engineering: Restraint, Slaughter and Bleeding
Controlled restraint
Head restraint, body positioning and access are configured around cattle size, throughput and the method accepted by your certifier. Rotary killing boxes give the slaughterman a stable position and reduce avoidable stress.
Bleeding time by design
Rail length, line speed and discharge location are calculated together. Dressing must not begin before the required bleeding interval is complete, and the line should make that interval visible to supervisors.
Stunning policy
We can integrate reversible, non-penetrating stunning, conventional stunning, or a no-stun workflow. The correct choice depends on the certifier and destination market, so it is fixed during process design rather than added later.
Hygiene, Separation and Traceability
Halal compliance is judged together with food safety. The line should keep clean and dirty operations physically separated, provide dedicated knife sterilization points, control the route of hides and offal, and prevent condensation or floor splash from returning to edible product. Stainless steel, smooth food-contact welds, radiused corners and drainage details all support the washdown and audit routine.
- Clear separation between pre- and post-slaughter zones
- Dedicated halal and non-halal operating periods where required
- Knife, apron and hand-wash stations at decision points
- Visible identification of approved carcasses and offal
- Controlled routing of hides, heads and digestive contents
- Cleanable rails, platforms, guards and control panels
- Documented equipment materials and component records
- Layouts, utility drawings and process descriptions for audit
Compliance Support by Market
| Market / authority | Typical engineering focus | Responsibility boundary |
|---|---|---|
| Indonesia: MUI / BPJPH | RPH workflow, Muslim slaughterman access, reversible stunning option, bleeding interval, separation and traceability | Equipment and process documentation support; certificate issued after audit by the competent body |
| Malaysia: JAKIM | Hygienic layout, dedicated utensils, cleanable surfaces, segregation, records and Muslim operator workflow | Design support for the client’s certification process; final approval remains with JAKIM |
| Kazakhstan: KAZHALAL and other bodies | Restraint and slaughter access, bleeding rail design, cold-chain coordination and documentation for local review | Project documents and equipment compliance support; certification is country- and body-specific |
| Uzbekistan and wider OIC markets | Market-specific layout, orientation, separation, material selection and export documentation | We align with the client’s nominated authority and do not substitute for its decision |
Capacity Configurations
20-60 heads/day
A step-by-step line with rail transfer and manual dressing. Suitable for regional supply, first-stage investment and a clear later expansion path.
60-200 heads/day
Powered bleeding and dressing rails, hide puller, synchronized evisceration and a controlled inspection rhythm.
200-500 heads/day
Higher-speed transfer, automated stations and integrated data points. Building height, utilities and cold-chain capacity become critical design limits.
What We Need Before Designing the Line
- Animal data: cattle breed, average live weight and weight range
- Capacity: heads per day, shift length and seasonal peak
- Method: no-stun or accepted stunning system, plus the certifier’s written requirement
- Building: plan, clear height, drainage points, floor levels and available construction work
- Utilities: voltage, frequency, water, steam, compressed air and wastewater capacity
- Product flow: carcass, head, offal, hide and waste destinations after slaughter
- Cold chain: chilling room capacity, target temperature and dispatch method
How We Reduce Project Risk
Halal cattle projects fail at interfaces more often than at individual machines. The certifier may approve a method, but the building may not provide enough rail length; the killing box may be correct, while the hide route crosses the clean side; or the chilling room may not absorb the rated slaughter speed. We surface those issues during process design, before drawings are frozen and before equipment enters production.
Each proposal identifies the capacity assumption, process method, equipment scope, customer responsibility, utility requirements, drawing deliverables and acceptance criteria. During manufacturing, agreed sections are pre-assembled and tested. Before shipment, test records and packing plans are reviewed. On site, commissioning verifies the line at increasing load until the agreed capacity and operating rhythm are stable. This structure keeps certification requirements, engineering decisions and commercial scope connected instead of treating them as separate workstreams.
From Drawing to Factory Acceptance Test
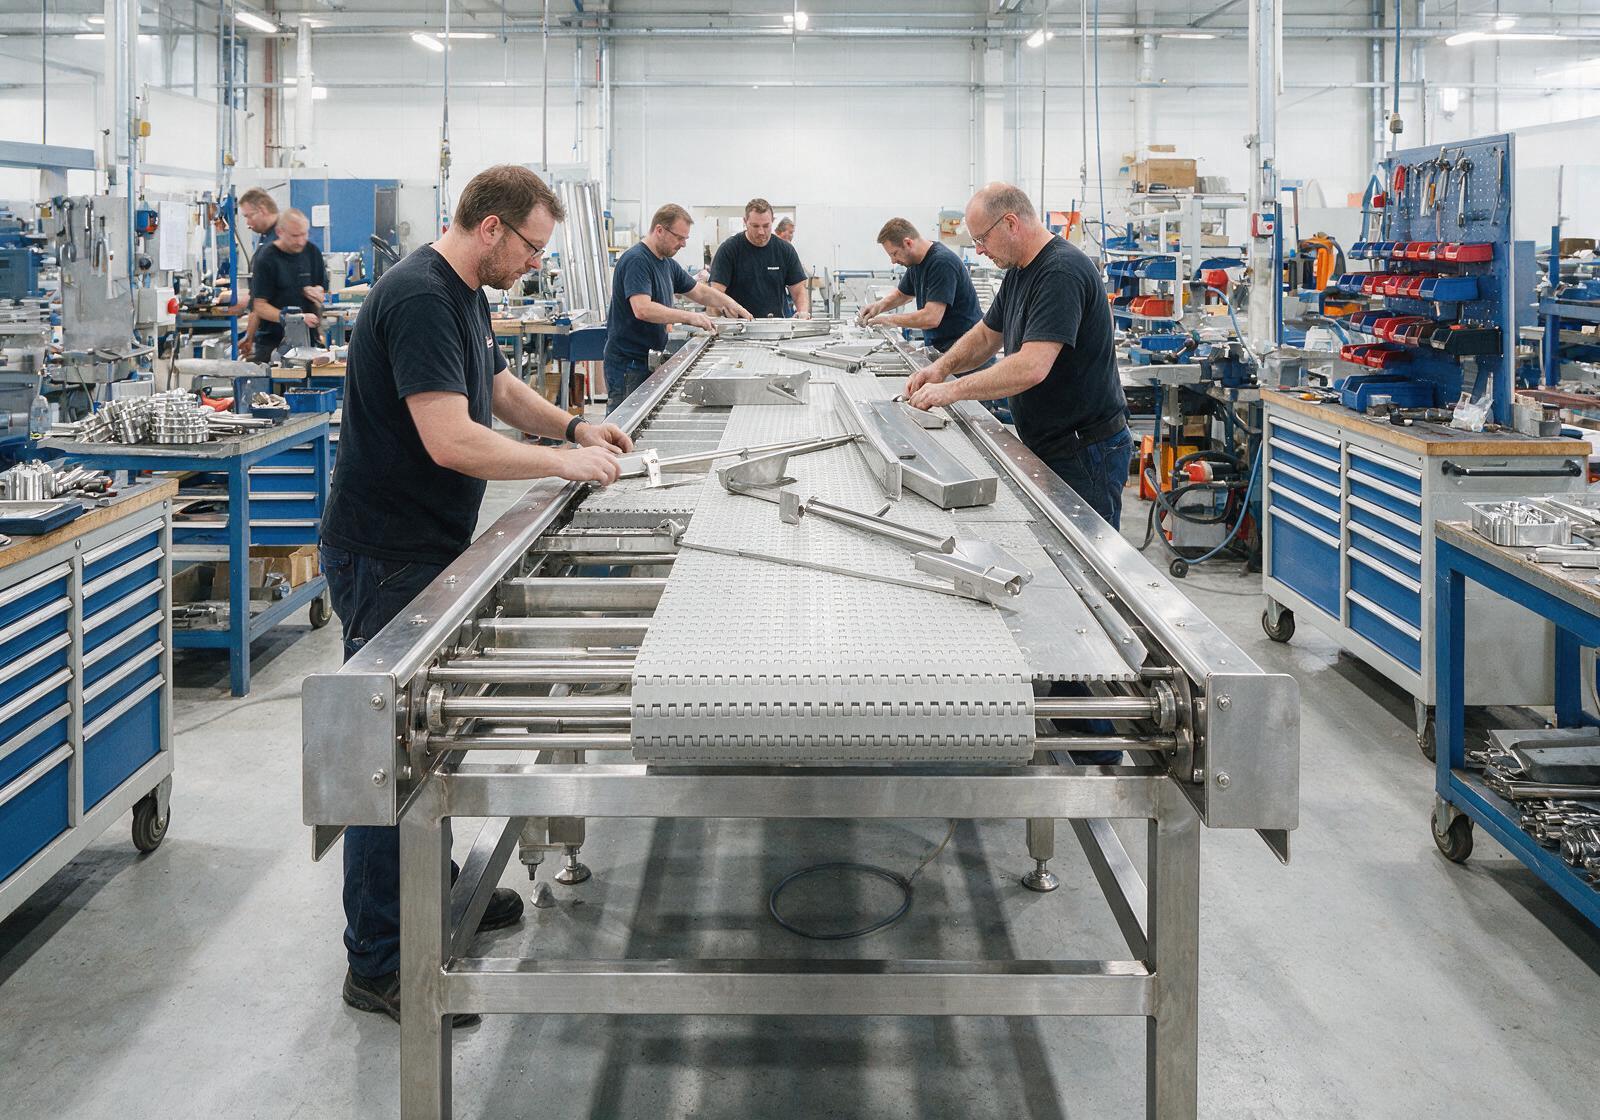
Once the process is agreed, we prepare the equipment list, rail routing and utility interfaces. Line sections are fabricated in our Nanjing workshop, pre-assembled where practical and tested before shipment. For turnkey projects, the customer can witness the factory acceptance test in person or by live video.
The same package can include installation, commissioning and operator training. The project boundary is written into the quotation so building works, refrigeration, boilers and utility connections remain clear rather than being discovered during installation.
Frequently Asked Questions
Is reversible stunning accepted for halal cattle slaughter?
Acceptance varies by country and authority. Some schemes allow a reversible, non-penetrating stun when the animal is alive at the time of slaughter; others require no stunning. We design to the written requirement from your certifier and do not make the religious ruling ourselves.
How long should the bleeding rail be?
Rail length is calculated from line speed and the required bleeding time, with allowance for discharge and inspection. The correct figure depends on the certifier, animal size and operating rhythm, so it is set during process design.
Can one plant process halal and non-halal cattle?
Yes, but separation must be engineered rather than assumed. Depending on the authority, the plant may need separate time windows, controlled cleaning, dedicated utensils and documented changeover procedures.
Do you provide certification for the equipment?
No single equipment certificate covers an abattoir’s halal status. We provide design information, material records, layouts and process documents for your certification audit. The recognized authority issues the final certificate after evaluating the plant and its operation.
Can the line be designed for later capacity expansion?
Yes. We can allow for longer rails, additional dressing stations, larger chilling capacity and utility headroom. The expansion plan should be stated before the first layout is frozen so the structural and space allowances are coherent.
What information is needed for a budget proposal?
Send cattle weight, heads per day, shift pattern, slaughter method, target certifier, building dimensions, voltage, water and steam data. These inputs let us return a process flow, equipment list and realistic budget range.
Plan the Line Around the Audit You Must Pass
Send the target market, capacity and certifier. We will identify the process decisions that must be fixed before equipment selection.